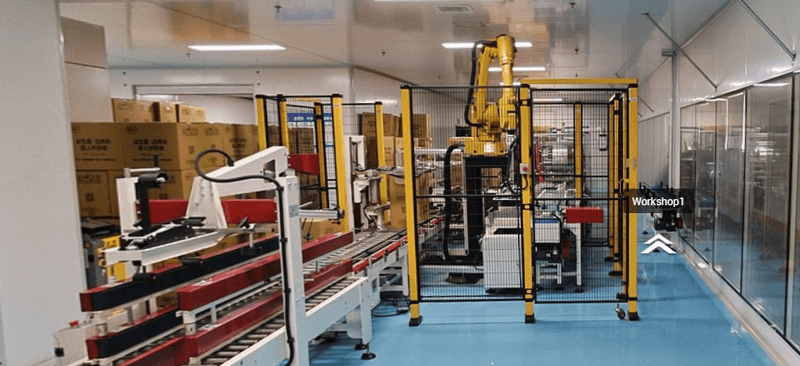
GMP‑compliant Full‑chain Manufacturing & Strain Bank
Our 40,000 ㎡ standardized GMP‑compliant manufacturing campus is equipped with over 200 professional fermentation tanks. We maintain a strain bank preserving more than 1,500 proprietary strains under liquid‑nitrogen storage.
We own complete in‑house production workflows including probiotic fermentation, centrifugation, freeze‑drying, powder blending and final packaging. Advanced micro‑encapsulation technology is applied to enhance strains’ resistance against gastric acid and bile salt, greatly improving survival rate during gastrointestinal transit and extending shelf‑life stability even under normal storage conditions. Strict production process control ensures batch‑to‑batch consistency for bulk strains and finished products.